Start with the drop, not the filler
Every cushioning decision answers two questions. How hard can the parcel land, and how much deceleration can the product survive? The first depends on the route. Parcel networks involve manual lifting, conveyor transfers and chutes, so a box may fall onto any face, edge or corner. Lighter parcels tend to be thrown and dropped from greater heights than heavy ones, simply because they are easier to handle.
The second question is about the product. Engineers describe fragility as the peak acceleration, usually in multiples of gravity, that an item can take before it breaks or stops working. ASTM D3332 describes how to measure it with a shock machine. Most small teams will never run that test, but the idea still helps: a glass vase, a laptop and a cast-iron pan have very different fragility levels, and they should not share the same cushioning recipe.
Reading a cushion curve
Foam suppliers publish cushion curves, typically produced following ASTM D1596. Each curve plots the peak deceleration a product receives against static loading, which is the product's weight divided by the area of cushion it rests on. Each curve applies to one thickness and one drop height.
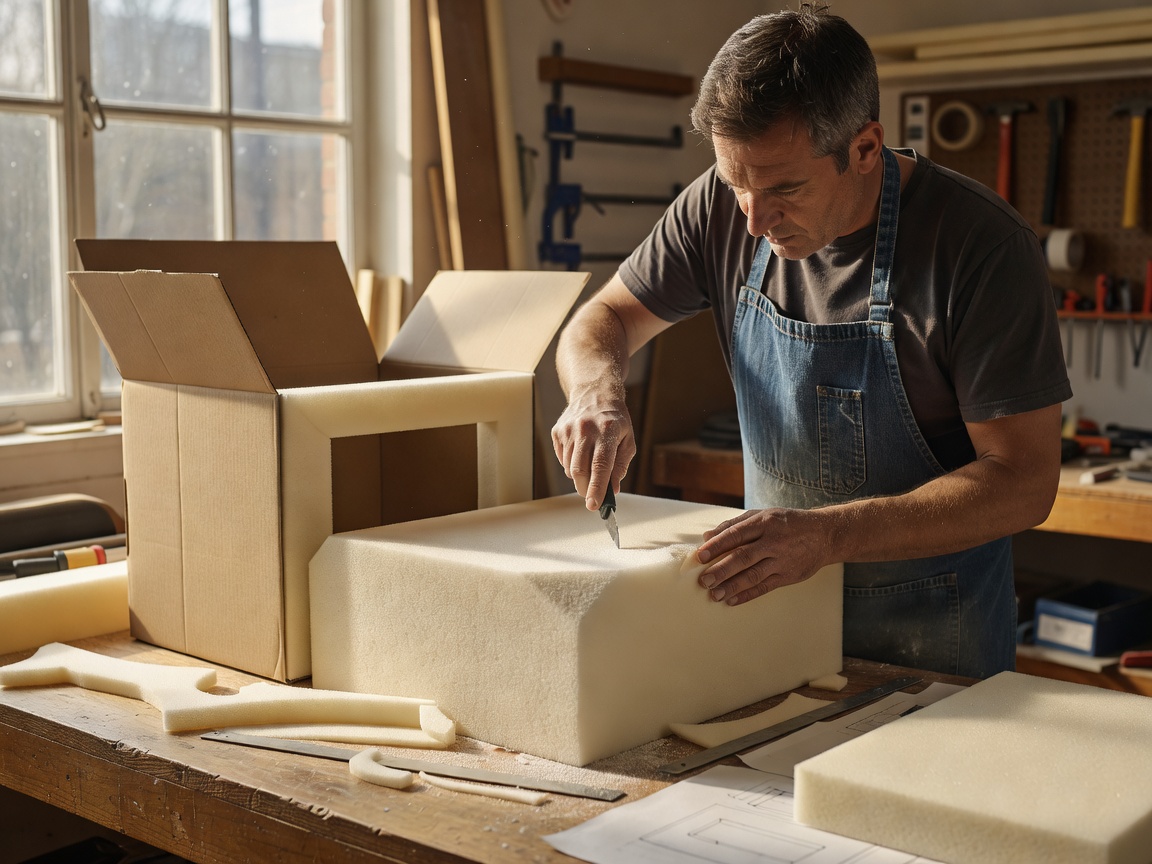
The curves have a characteristic dip. With too little bearing area, the static load is high, the foam compresses completely and the product "bottoms out" against the hard wall. With too much area, the foam barely compresses and behaves almost like a solid block, passing the shock straight through. The lowest point of the curve is the sweet spot. This is why a large slab of foam can protect worse than four carefully sized corner blocks.
For void fill and paper cushioning, formal curves are rarer, so design by principle: enough depth on every side, firm contact so the product cannot migrate, and confirmation through drops.
Common cushioning materials compared
Suspension, retention and corners
Good cushioning holds the product away from every wall, keeps it from shifting and puts extra protection where impacts concentrate. Corner and edge drops are the most damaging because the box lands on a tiny contact area and the product tends to rotate toward the impact. Corner blocks, edge rails and suspension trays address that directly.
Retention matters just as much. Loose fill that is perfect at the packing bench can settle during hours of vibration and leave a gap above the product. Once there is space to move, the product becomes a hammer inside its own box. Many carrier packing guides suggest around 5 cm (2 in) of cushioning between a fragile item and each wall, and they emphasise filling voids so nothing shifts when the box is shaken.
Vibration and resonance
Cushions behave like springs, and every spring-and-mass system has a natural frequency. If road or conveyor vibration matches it, the product can bounce more inside the pack than the vehicle itself moves. Random vibration testing under ASTM D4728 or within ISTA sequences exposes this. Remedies include changing cushion thickness or bearing area, which shifts the natural frequency, and firmer retention so parts cannot rattle.
A bench routine for cushioning
- Classify the product: rugged, moderate or fragile, and note its weakest point.
- Decide the clearance on all sides and protect corners and edges first.
- Choose a material that suits the number of impacts expected, not just the first.
- Check static loading against supplier curves where available.
- Pack, close and shake; then drop on faces, edges and corners and inspect.
- Remove material where tests show surplus. Space you do not need costs postage.